Epoxy Systems
Three product lines, one epoxy floor. MavClad EM troweled mortar builds the floor, MavCoat coatings — SLE self-leveling, HB high-build, PC broadcast, Metallic — finish it, and MavPrime EP bonds the whole system to the slab. Seamless, chemical-resistant, 100% solids epoxy, formulated and installed by the same company.
System Overview
One Chemistry. Three Lines. Zero Seams.
Every Maverick epoxy floor is built in the same order. MavPrime goes down first — MavPrime EP penetrating epoxy primer over mechanically prepared concrete, or MavPrime MVT where the slab is green or moisture-tolerant priming is specified. MavClad builds the floor — MavClad EM is the ¼″ trowel-applied epoxy mortar that carries heavy-duty traffic, chemical exposure, and mechanical abuse on the plant floor. MavCoat is the epoxy coating over it — self-leveling MavCoat SLE, high-build MavCoat HB, a MavCoat PC silica broadcast for texture, or MavCoat Metallic for customer-facing space — and on lighter-duty floors a MavCoat build is the floor.
The system is sealed last: a pigmented MavSeal UPA grout coat over MavClad EM, or MavCoat CES clear epoxy siloxane over broadcast and decorative builds. Every layer traces to its own Maverick data sheet or system guide — specified to your floor.
Why Facilities Specify Maverick Epoxy
- Verified film build — 100% solids means what we apply is what cures. No solvent loss, no shrinking films, no guesswork.
- Chemical resistance — stands up to oils, coolants, alkaline cleaners, and intermittent acid splash common in plant environments.
- Seamless and cleanable — no grout lines, no joints in the wear surface, no place for contamination to live.
- Built to the duty, not to a mil count — a ¼″ MavClad EM mortar where forklifts and impact live, a MavCoat coating where they don’t.
- Repairable for life — damaged areas are abraded and recoated; the floor never has to come out.
- Safety striping and demarcation — aisle lines and zone colors are coated into the system, not painted over it.
System Build-Up
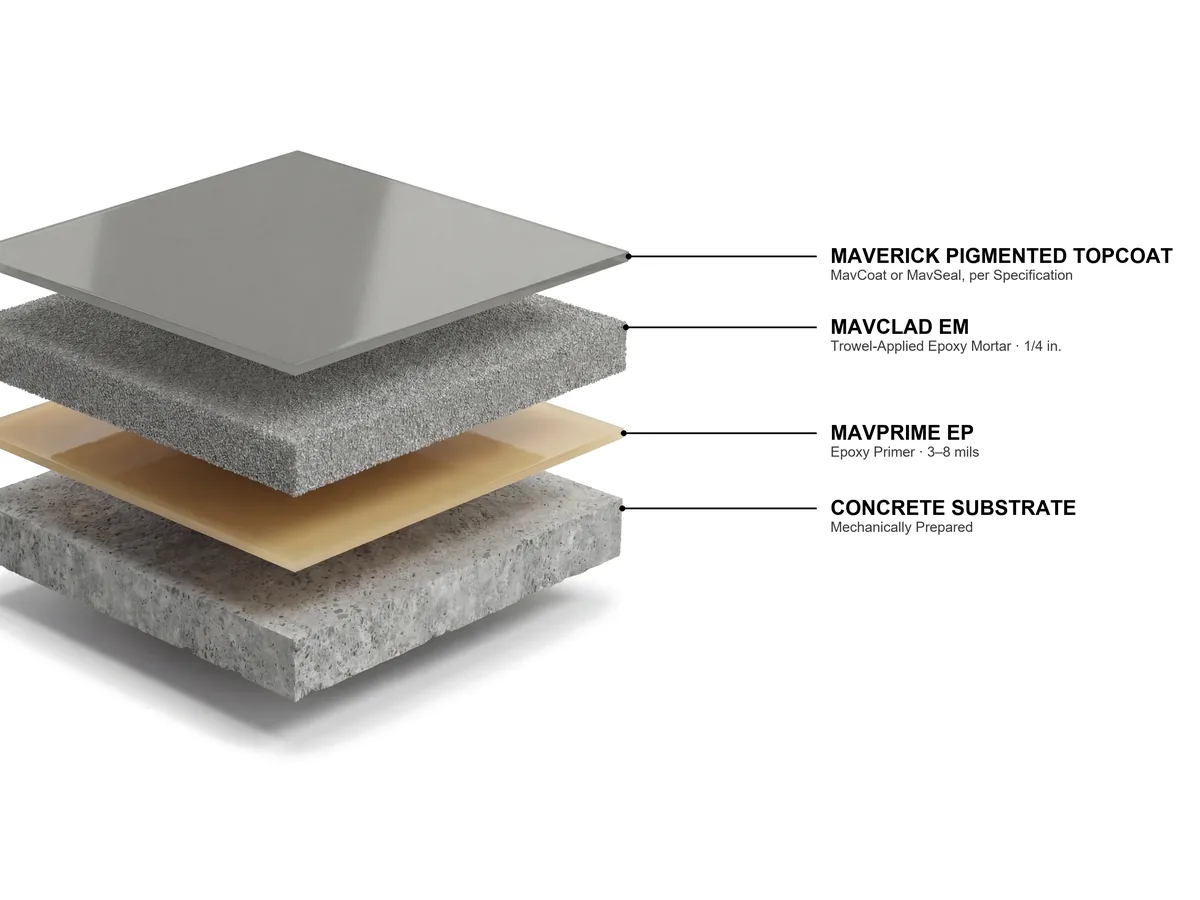
Epoxy System Cross-Section
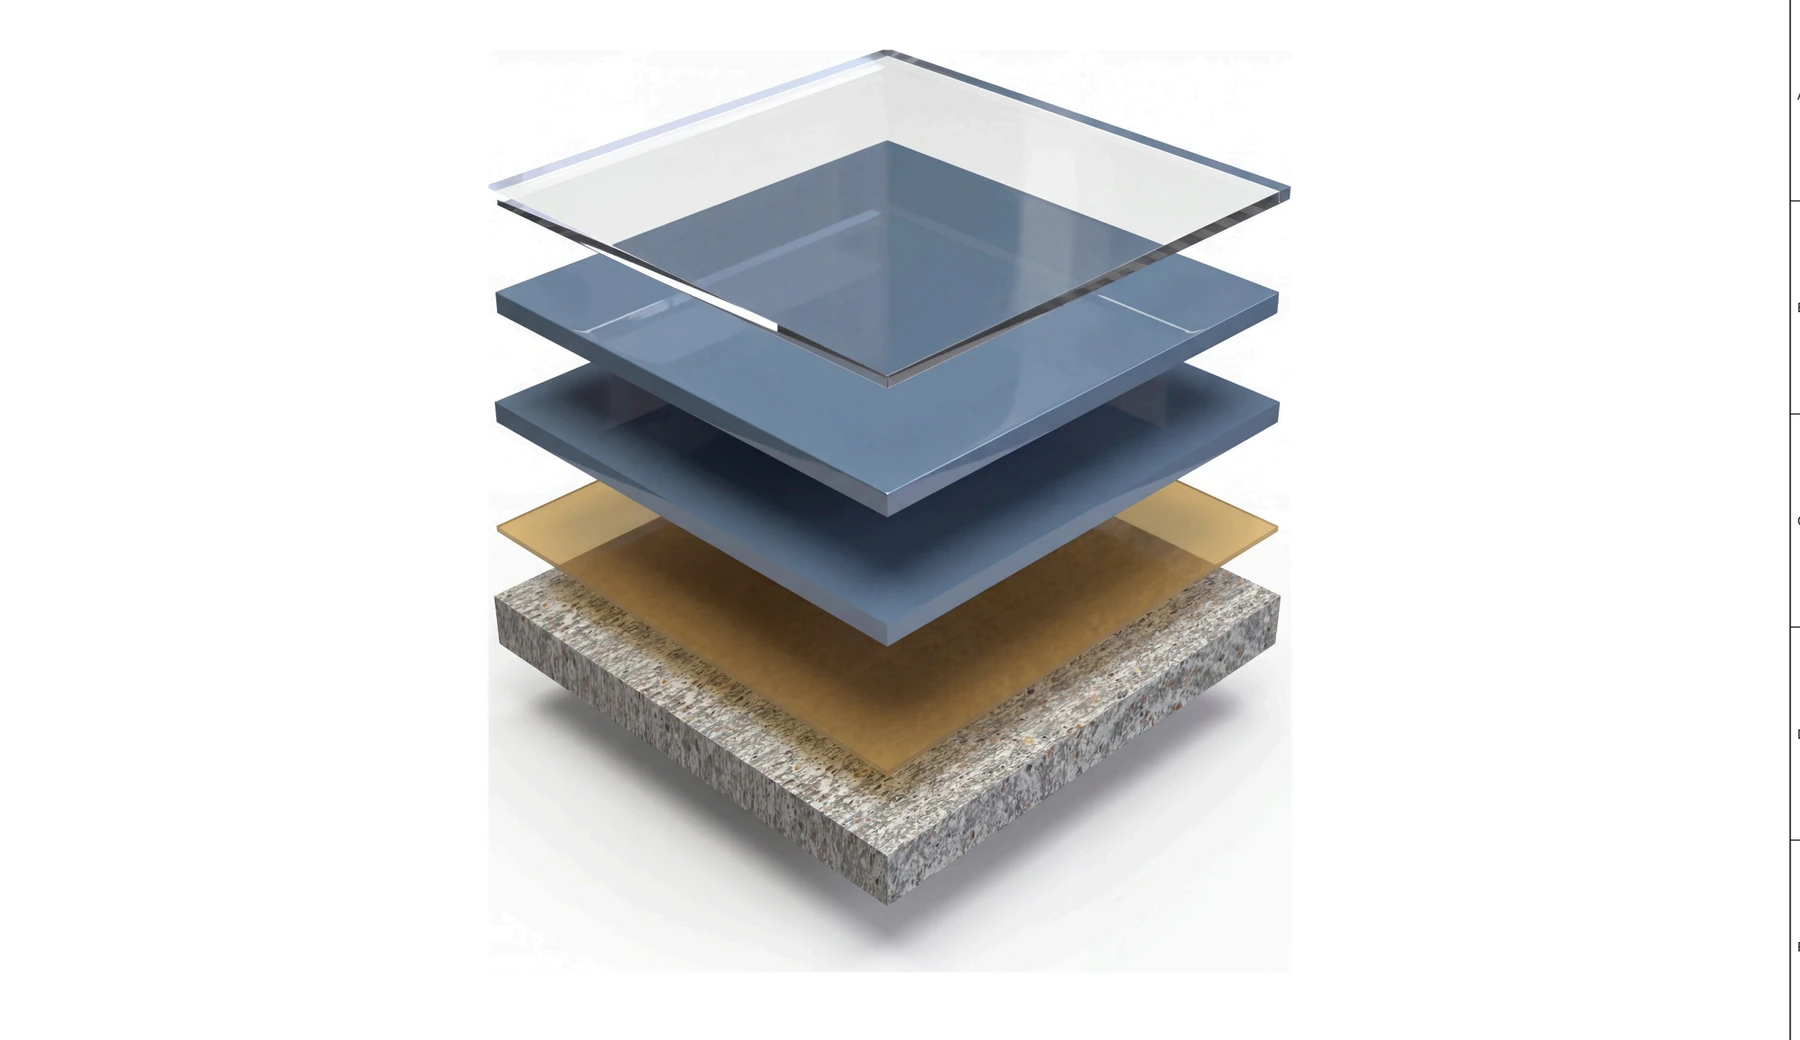
The standard MavCoat SLE self-leveling build-up over MavPrime EP. For heavy-duty floors the body is MavClad EM troweled mortar at a full ¼″ — see the MavClad systems page and its shop drawing below. MavCoat PC adds a silica broadcast and a MavSeal UPA polyaspartic topcoat, and MavCoat Metallic adds a MavCoat CES epoxy siloxane topcoat; thicknesses adjust per the project data sheet.
System Components
Every Component, Documented
The products that make up the system, what each one does, and where to get its technical data. Components are supplied as factory-batched kits and installed by Maverick crews per the project specification.
| Application | Product | Function in the System | Documents |
|---|---|---|---|
| Primer | MavPrime EP | Penetrating 100% solids epoxy primer over CSP 3+ prepared concrete — the bond coat under every Maverick epoxy system. | TDS (PDF) |
| Moisture-tolerant primer | MavPrime MVT | Moisture-tolerant epoxy primer — specified in place of MavPrime EP for green concrete, per the MavClad EM data sheet. | Data Sheet (PDF) |
| Troweled mortar body | MavClad EM | ¼″ trowel-applied 100% solids epoxy mortar — the floor itself on heavy-duty industrial traffic without thermal shock; fills coves, keyways, and chases. Finished with a pigmented MavSeal UPA grout coat. | Data Sheet (PDF) |
| Self-leveling body | MavCoat SLE | Self-leveling 100% solids epoxy coating — the workhorse MavCoat build for plant floors; also the broadcast-receiving basecoat. | TDS (PDF) |
| High-build body | MavCoat HB | 2-layer system per its guide — epoxy primer (3–8 mils) plus 100% solids self-leveling epoxy body (10–30 mils), pigmented on-site with MavTints. | System Guide (PDF) |
| Decorative body | MavCoat Metallic | Metallic pigmented epoxy body in 35 standard blends. | Metallic Colors |
| Clear sealer | MavCoat CES | Clear epoxy siloxane topcoat — the protective satin or gloss finish over broadcast and decorative builds. | TDS (PDF) |
| Topcoat | MavSeal UPA | Pigmented or clear polyaspartic finish coat selected per service environment — the grout coat over MavClad EM and the topcoat over MavCoat PC broadcasts. | Color Charts |
Finish Options
From Plant Floor to Showroom
Same primer, same epoxy chemistry — the body and finish are tuned to the duty.
MavClad EM — Troweled Mortar
The heavy-duty floor: a ¼″ trowel-applied 100% solids epoxy mortar over MavPrime EP, sealed with a pigmented MavSeal UPA grout coat. Warehousing, manufacturing, chemical processing, traffic aisles and assembly lines — gloss, orange peel, or satin finish. MavClad systems page.
MavCoat SLE — Self-Leveling
High-build 100% solids self-leveling epoxy coating. Smooth, seamless, and chemical-resistant — the default MavCoat build for production floors, warehouses, and maintenance bays. Safe for incidental food contact per its PDS, with colors matched through the MavTints universal tinting system.
MavCoat PC — Prime & Coat
A 1/16 in. slip-resistant system: MavPrime EP primer, a MavCoat SLE epoxy basecoat with a single silica-sand broadcast, and a MavSeal UPA polyaspartic topcoat for manufacturing floors and tough-traffic areas.
MavCoat HB Epoxy — High Build
High-gloss 2-layer epoxy system per the MavCoat HB Epoxy system guide — epoxy primer plus a 100% solids self-leveling body that restores eroded floors, with optional high-wear topcoats.
MavCoat Metallic
Premium metallic epoxy with flowing three-dimensional visual effects, moved while wet for one-of-a-kind depth. Showrooms, lobbies, and retail floors that need to impress and still take traffic.
Where It Performs
Built for These Environments
- Manufacturing
- Warehousing & Distribution
- Automotive & Aviation
- Laboratories
- Healthcare Support Areas
- Showrooms & Retail
- Maintenance Bays
- Vivariums
- Petrochemical
- Wastewater
- Municipal Facilities
Performance
Typical System Properties
MavClad EM — Troweled Epoxy Mortar
| Property | Test Method | Typical Value |
|---|---|---|
| Typical application | — | ¼″ trowel-applied topping |
| Compressive strength | ASTM C579 | 13,250 psi |
| Tensile strength | ASTM D638 | 8,650 psi |
| Flexural strength | ASTM C580 | 5,000 psi |
| Bond strength | ASTM D4541 | 350 psi |
| Hardness, Shore D | ASTM D2240 | 75–90 |
| Abrasion resistance, CS-17 wheel, 1,000 cycles | ASTM D4060 | 75 mg loss |
| VOC content | — | 0 g/L, 100% solids |
| Surface profile | ICRI 310.2R | CSP 3–5 |
| Foot traffic | 77°F | 12–24 hours |
| Light service | 77°F | 24 hours |
| Full service | 77°F | 48–72 hours |
MavCoat SLE — Self-Leveling Epoxy Coating
| Property | Test Method | Typical Value |
|---|---|---|
| Compressive strength | ASTM D695 | 11,600 psi |
| Tensile strength | ASTM D638 | 9,600 psi |
| Flexural strength | ASTM D790 | 12,800 psi |
| Bond strength to concrete | ASTM D7234 | > 400 psi (substrate failure) |
| Hardness, Shore D | ASTM D2240 | 75 |
| Abrasion resistance, CS-17 wheel, 1,000 cycles | ASTM D4060 | 50 mg loss |
| VOC content | EPA Method 24 | 100% solids system |
| Return to service, light foot traffic | Standard / slow / fast activator | 10 / 16 / 6 hours |
| Return to service, full chemical cure | — | 5 days |
Chemical Resistance
Ratings for MavCoat SLE, the 100% solids self-leveling epoxy coating, from its product data sheet. Tested on fully cured material. E = Excellent · G = Good · F = Fair · NR = Not Recommended. An asterisk means staining is the only defect.
| Reagent | Rating | Reagent | Rating |
|---|---|---|---|
| 10% Acetic Acid | G | Methyl Ethyl Ketone | G |
| Vinegar | G | Xylene | F |
| 10% Citric Acid | G | Ethylene Glycol | G |
| 10% Hydrochloric Acid | G | Isopropyl Alcohol | F |
| 30% Hydrochloric Acid (muriatic) | G | Mineral Spirits | E |
| 10% Nitric Acid | G* | Brake Fluid | F |
| 50% Phosphoric Acid | F | Transmission Fluid | E |
| 10% Sulfuric Acid | G | Motor Oil | E |
| 37% Sulfuric Acid | F | 50:1 Gas/Oil Mixture | E |
| 70% Sulfuric Acid | F | E85 Gasoline | E |
| 20% Ammonium Nitrate | E | E95 Gasoline | E |
| 20% Sodium Chloride | E | Unleaded Gasoline | G |
| 50% Sodium Hydroxide | E | Skydrol | E |
| Betadine | G* | Coffee | E |
| Bleach | E | Cola | E |
| Urine | E | Ketchup | G |
| Red Wine | E | Mustard | G |
FAQ
Common Questions
How thick is a Maverick epoxy floor?
It depends on the duty. MavClad EM, the heavy-duty troweled epoxy mortar, is placed at a full ¼″. A MavCoat SLE self-leveling coating build is 16–30 mils nominal, and MavCoat HB is a 2-layer build — epoxy primer at 3–8 mils plus a 100% solids self-leveling body at 10–30 mils.
How soon can an epoxy floor return to service?
MavClad EM takes foot traffic in 12–24 hours and full service in 48–72 hours at 77°F. A MavCoat SLE coating takes light foot traffic in 10 hours with the standard activator (6 hours fast, 16 hours slow) and reaches full cure in 5 days at 72°F / 50% RH. Request the data sheets for project values.
What chemical exposure can Maverick epoxy handle?
MavClad and MavCoat epoxy stand up to oils, coolants, alkaline cleaners, and intermittent acid splash common in plant environments. For repeated hot washdown and thermal shock service, epoxy is not the answer — that is where MavCrete cementitious urethane comes in.
How does surface preparation work?
Every Maverick epoxy system starts with mechanically prepared concrete — grinding, repairs, and patching before a drop of resin goes down — followed by a penetrating coat of MavPrime EP over the CSP 3+ profile (MavPrime MVT on green concrete), the bond coat under every MavClad and MavCoat system.
Related Products
What Goes Into the System
MavPrime
MavPrime EP
High-solids penetrating epoxy primer engineered for concrete substrates. Deep mechanical bond into the profile with excellent moisture tolerance — the foundation layer under every MavClad and MavCoat floor.
View in Catalog
MavCoat
MavCoat CES
Clear epoxy siloxane topcoat — two-component, high-solids, isocyanate-free — protecting broadcast and decorative builds with an abrasion-, chemical-, and UV-resistant satin or gloss finish.
View in Catalog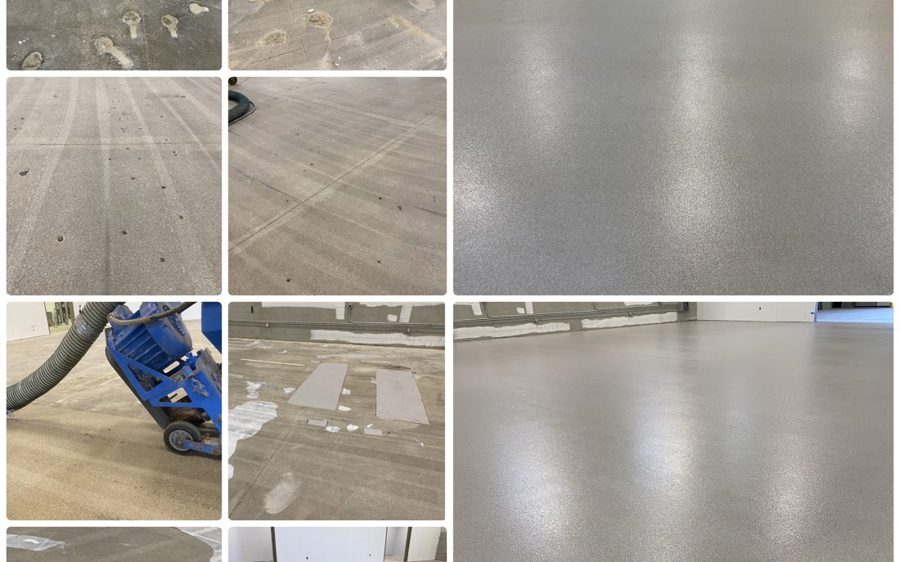
MavPatch Epoxy
Epoxy-based patching compound for concrete repair. Restores spalls, pop-outs, and failed joints to structural performance before the coating system goes down, so the finished floor reads as one surface.
View in Catalog
MavJoint
MavJoint JF
Semi-rigid joint filler in six standard colors to honor moving joints through the new floor while protecting joint edges from wheel traffic.
View in Catalog
Shop Drawings
Isometric Shop Drawings — Epoxy Systems
Formal isometric shop drawings for every Maverick epoxy build-up — MavClad EM mortar and the MavCoat coating systems, layer by layer, ready for the project file. Direct download, no gating. The full 18-drawing standard library lives in the Architect Center — or build any custom combination in seconds with the System Builder.
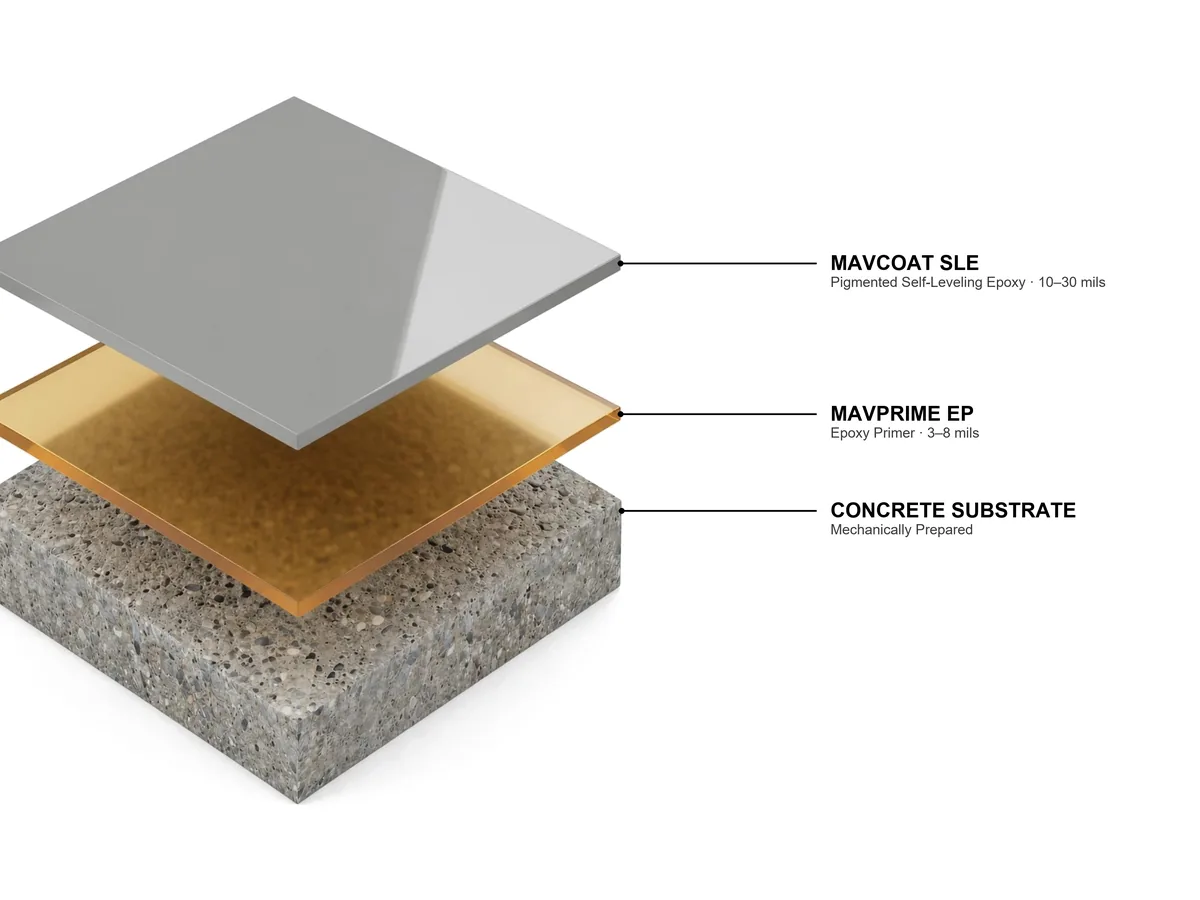
MavCoat SLE
Download PDF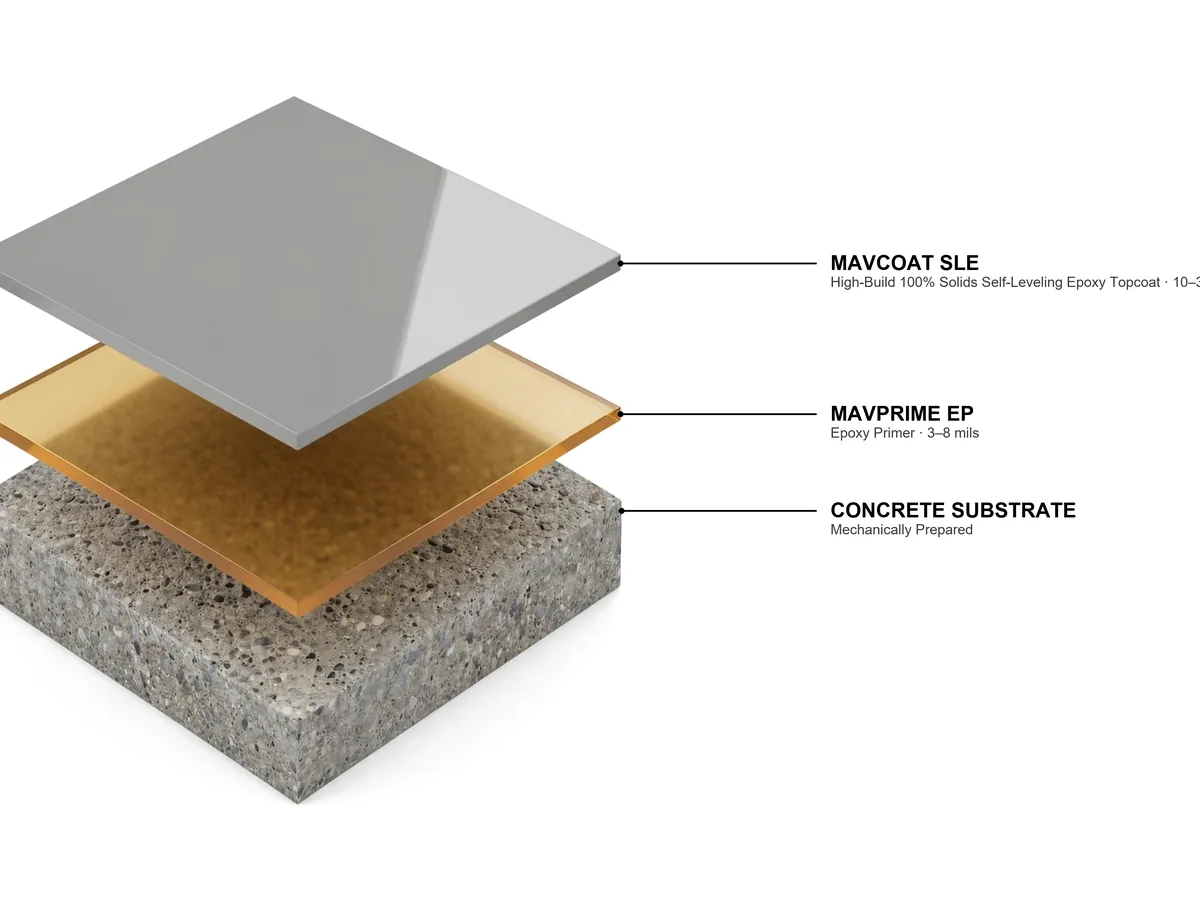
MavCoat HB
Download PDF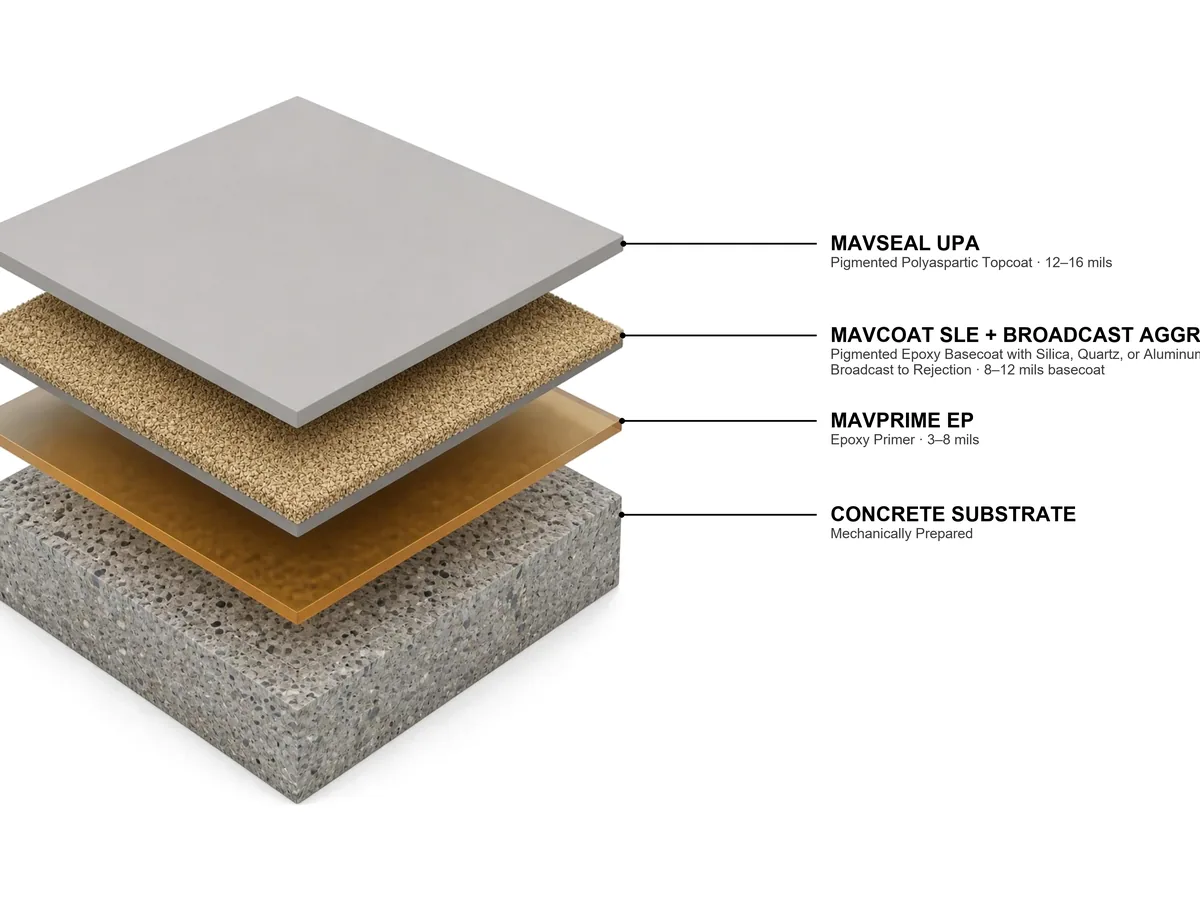
MavCoat PC
Download PDF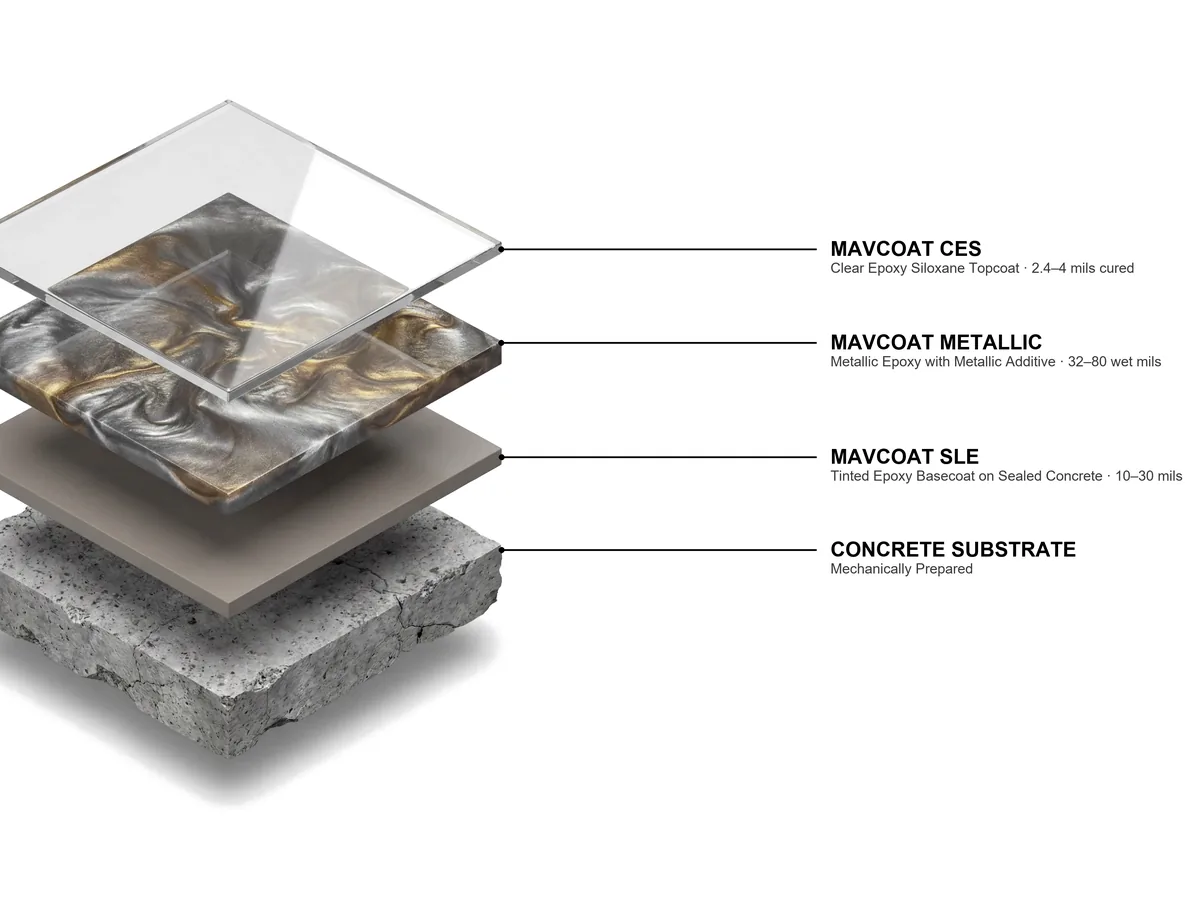
MavCoat Metallic
Download PDF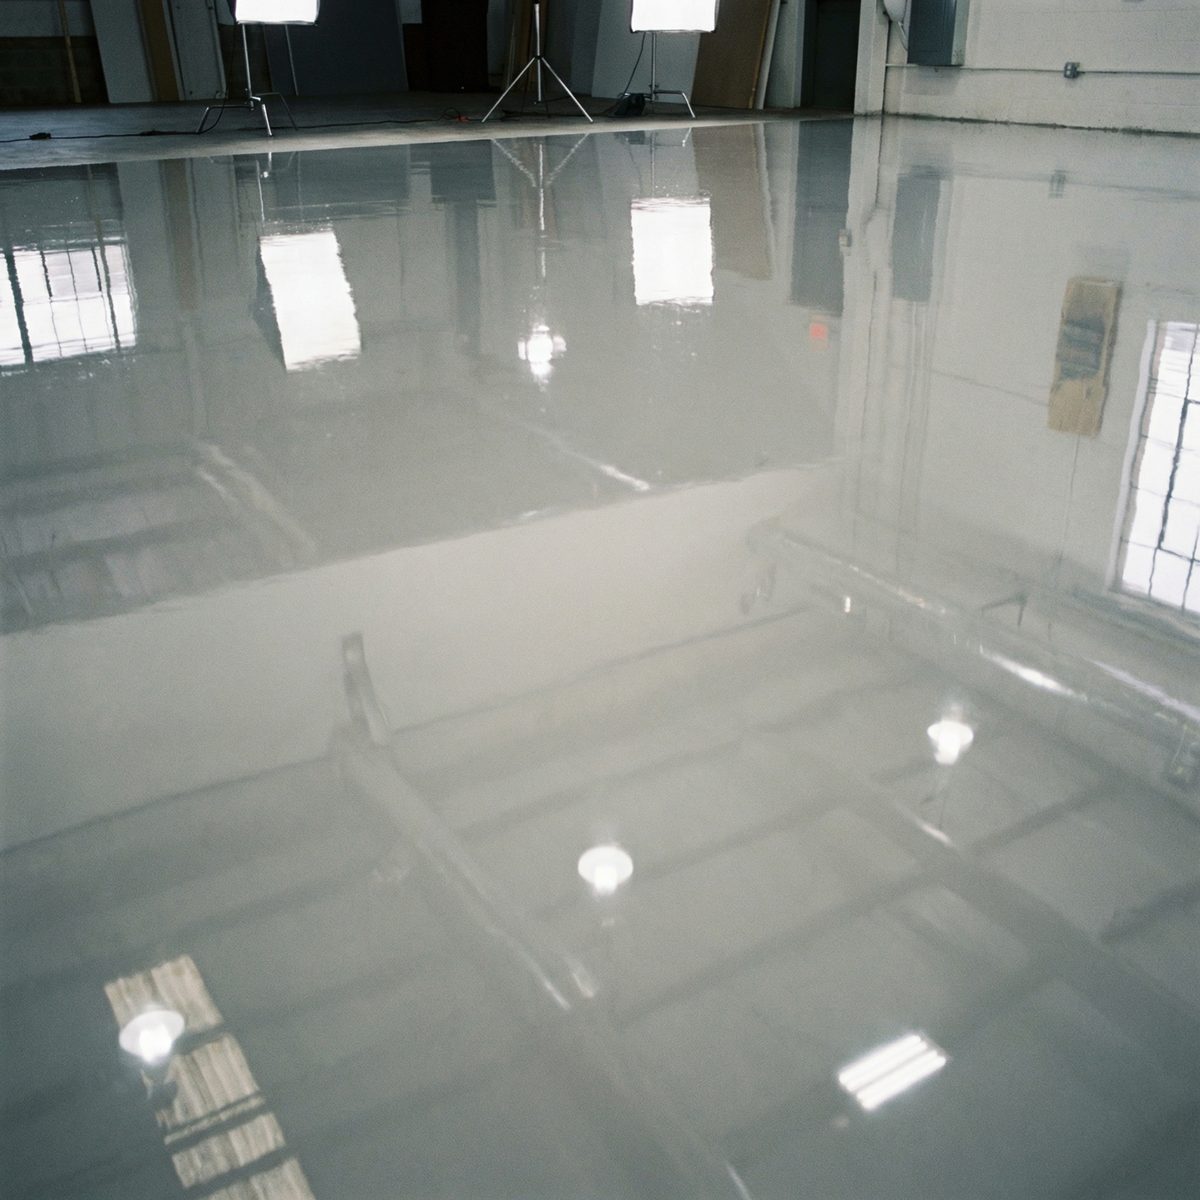
The Finish, Up Close
A properly placed MavCoat SLE coating reads like glass — a seamless, light-reflective surface that brightens the facility and shows exactly how flat the placement is. Gloss like this is the product of substrate preparation, primer discipline, and a crew that screeds to tolerance.
For Specifiers
Details & Specifications, Ready to Drop In
The Architect Center carries the full MAV-EP detail series — cove bases, drain transitions, terminations, and joint treatments for epoxy systems — plus the CSI 3-part specification under Division 09, Section 09 67 23 Resinous Flooring.
The Maverick Difference
From Prep to Finish
Most floor failures are prep failures. Ours start with the grinder — mechanical preparation, repairs, and patching before a drop of resin goes down.
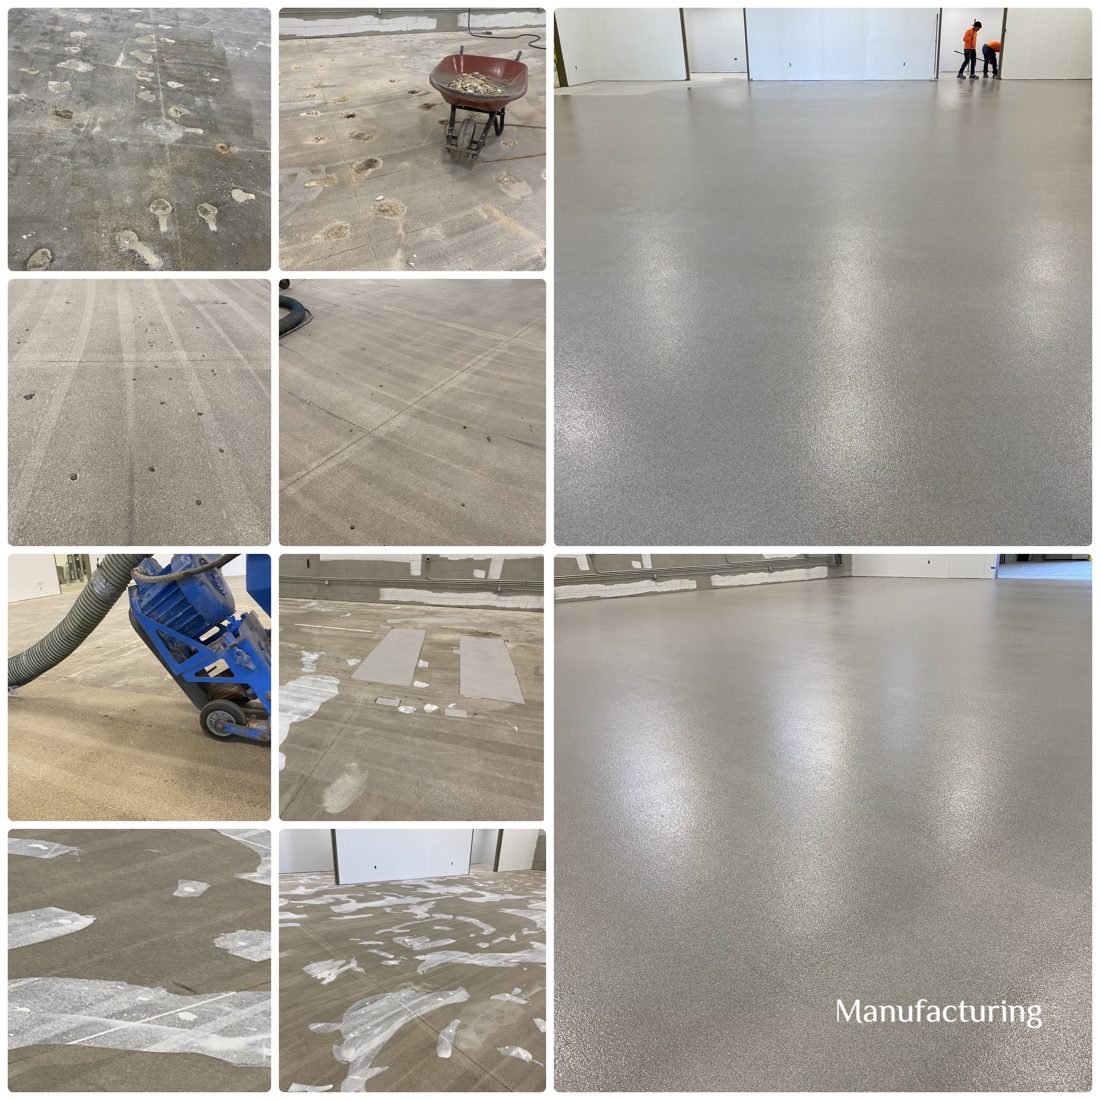
Grind, repair, patch — then the system: a manufacturing floor from prep to finish
Scope an Epoxy Floor
Tell us the square footage, traffic, and exposure. We'll respond with a recommended MavClad or MavCoat build-up and budget range within 48 hours.